Syatirah Mohd Noor1.2, Mohamad Kamarol Mohd Jamil1 , Nor Asiah Muhamad3.1, Sharin Ab Ghani4 dan Khairul Anwar Abdul Halim5
1 School of Electrical and Electronic Engineering, University Sains Malaysia (USM), Engineering Campus, Nibong Tebal, Pulau Pinang 2Faculty of Electrical Engineering and Technology, University Malaysia Perlis (UniMAP), Pauh, Perlis 3 Department of Electrical and Electronic Engineering, Faculty of Engineering, Universiti Teknologi Brunei (UTB),Tungku Highway BE1410 Gadong, Brunei Darussalam 4Faculty of Electrical Engineering, Universiti Teknikal Malaysia Melaka (UTeM) Melaca, Malaysia 5 Faculty of Chemical Engineering, University Malaysia Perlis (UniMAP), Pauh, Perlis *Corresponding author : eekamarol@usm.my
Abstract: Several researchers are investigating the polymer nanocomposite usage as electrical insulating materials since it has attracted their attention. The aims are to determine an appropriate nanocomposite blending for the optimization of the dielectric insulation performance. Extruding is one of the main process in blending the composite material. The ideal blends with mixed nanofillers are determined using a conventional technique like the onefactor-at-a-time (OFAT) method. This traditional method required a large number of samples to achieve the blended optimization that could increase the time and cost. In this work, Design of Experiment (DOE) method was used to find the optimization of compounding process using The Two-Level Factorial. The new insulation material contains linear low-density polyethylene (LLDPE) and high-density polyethylene (HDPE) blends with aluminium oxide (Al2O3) nanofillers being tested in this study. The research on employing compounding polymer-based nanocomposite as a high voltage direct current (HVDC) cable insulating material is presented. In this research, the sample is compounded with twin screw extruder that need 3 factors to be set which are: the concentration of the material, rotation per minute of screw speed and the temperature of the machine. The conductivity of the blended samples is measured and analyzed. The crystallinity of the samples also being tested to see the effect of the compounding process. Trough the DOE approach, eight samples are required to be produced to find the optimization in compounding process. The results found that there is enhancement in the conductivity and performance of the samples by optimizing the concentrations of nanofillers to the LLDPE/HDPE-Nanocomposite. This saves a great deal of time and money in contrast to the command approach, which is a one-of-the-time (OFAT) method. Weightage has the most noticeable impact on the sample's conductivity, as shown by the DOE results, which show a percentage contribution of 73.67%. The response surface plot indicates that the optimal weightage concentration and temperature for the LLDPE/HDPE-Alumina that yields the lowest conductivity level are 5wt% and 180OC, respectively. It can be concluded that DOE is a feasible alternative to determine the optimum processing condition using twin screw extruder in sampling the compounding of LLDPE/HDPE-Alumina, which in turn, helps improve the conductivity of these polymer nanocomposite with the low conductivity value.
Keywords: Polymer blends, Conductivity, nanofiller, design of experiments, optimization
Received: March 14th, 2024. Accepted: June 26th, 2024
DOI: 10.15676/ijeei.2024.16.2.6
1. Introduction
Extruded polymeric HVDC cable has a short development history and has demonstrated significant power transfer improvements over HVAC cable. Since the 1950s, when the first 110 kV extruded polymeric HVAC cable was created, polymeric insulation material has been incorporated into HVAC cables on a large scale. The first commercial polymeric HVDC cable was placed into service in 1999, yet the development of HVDC cables lags much behind that of HVAC cables. The development of HVDC cables is currently the focus of study due to its shown superiority over HVAC cables in power transmission. Polymeric HVDC cables are developing quickly not only because of the previously listed benefits but also because of the increased requirements of contemporary power transmission. The main constraints on the development of contemporary power systems have been those related to safety, dependability, efficiency, and environmental friendliness. Polymeric HVDC cables are becoming more and more in demand, and their range of applications is growing.[1]
THE second generation of mixed resins, polymer nanocomposites (PNCs), are polymers loaded with a substantial quantity of nano-sized inorganic fillers (about 50% weight percent). Low manufacturing energy use and a decrease in greenhouse gas emissions over the whole life cycle, thermoplastic polymer blend material demonstrates positive characteristics as a prospective eco-friendly cable insulation material. As a result, many researches had been carried out to assess its performance as an alternative for cable insulation material. An enhanced polyethylene blend's isothermal crystallisation process reduced electrical tree growth and increased alternating current (AC) ramp breakdown strength. The influence of polymer nanocomposites has dominated the major research effort to far. Interfaces are dominant in this architecture. It was discovered that partial nano structuration of polymer nanocomposites improved partial discharge resistance, suppressed space charge production and affected charge relaxation, and increased treeing lifetime. In many circumstances, it is unclear how many attributes can be changed for the better at the same time. This is especially significant in two industrial applications where a material must meet a set of requirements. Chemical, mechanical, and thermal properties, for example, are examples of non-dielectric qualities. As a result, dielectric characteristics can be tailored, but only to increase overall performance in particular cases. [2]
A blend of polymers and a minuscule number of nano-fillers make up newly produced polymer nanocomposites. While having a lower concentration (a few weight percent), nanofillers have a substantially higher surface area than micro-fillers. As a result, in order to gain a fundamental understanding of the changes in dielectric characteristics caused by nanostructuring, it is imperative to look at the interactions between nano-fillers and polymer matrices. The maker should decide the precise scope and character of development work and studies, which may include a review of the materials and procedures used. Typically, such analyses would involve space charge measurements, breakdown tests, and electrical resistivity studies. [3].
Recently, it has been found that materials made of thermoplastic polyethylene have potential as HVDC cable insulation. Zhang et al. discovered in thin film studies that specific LLDPE/HDPE blends have greater DC breakdown strengths than specific XLPE. Researcher discovered that a 70 percent LLDPE with 30 percent HDPE blend outperforms cross-link polyethylene (XLPE) cable insulator in terms of mechanical and electrical characteristics of temperature dependence and conductivity [4]. In their study of the DC performance of polyethylene blends and related mini-cables, Vaughan et al. discovered that these materials outperform XLPE in terms of DC breakdown strength. There are currently no studies on temperature characteristics of DC performance, which is one of the most crucial criteria for HVDC cable design at high temperatures during operation, despite recent research suggesting the potential for thermoplastic polyethylene blends as HVDC cable insulation materials.[5] Due to the synergistic benefits of the mixing process (working together for larger outcomes, by mixing nanoscale fillers with polymers, strong materials might be produced. The fillers used in the polymer-based matrix are only used in limited amounts, usually less than 10% by weight.
All nanocomposites exhibit much better thermal stability than virgin LLDPE due to reductions in the effective activation energy throughout the degradation process. [6]
The PNCs have undergone significant development for a variety of uses. To create nextgeneration materials with great performance and several functions, polymer/clay nanocomposites must be manufactured. Effective dispersion and exfoliation of the composite layers into individual platelets in the polymeric matrixes determine how much performance is improved. [7]
According to Dennis et al., the kind of melt processing conditions had an effect on how much exfoliation occurred in nanocomposites made of organoclay. They also suggested that the type of extruder and the shape of its screws had an impact on the degree of delamination and dispersion of layered silicate nano-composites by melt compounding. The most successful melt-processing method for the exfoliation, intercalation, and dispersion of silicate layers has been found to be twin-screw extrusion. [8]
It is known that a network of chemical-physical interactions takes place when an organic matrix disperses a very low ratio of inorganic particles with at least one dimension smaller than 100 nm. This network of interactions causes a considerable adjustment in the material's macroscopic properties. Improvements in several of the most important characteristics of organic dielectrics, such as thermal stability and mechanical strength, can result from this. Moreover, it has greatly improved electrical characteristics including resistivity and insulator breakdown strength. The majority of earlier studies employed morphological analyses, breakdown strength tests, space charge generation, and dielectric loss experiments to evaluate the electrical characteristics of polymer nanocomposite. These dielectric measurements, however, fall short since they don't account for conductivity fluctuations, polarisation currents, or depolarization currents. It is impossible to pinpoint the reason of insulator degradation without proper information on these factors. [9]
Since these systems offer improved performance characteristics compared to the unmodified resin, such as increased swelling resistance, enhanced ion conductivity, decreased flammability, increased tensile strength and moduli, decreased thermal expansion coefficient, decreased gas permeability, increased swelling resistance and increased crystallinity, scientific research has focused a lot of attention on polyamide/layered silicate nanocomposites over the past ten years.[10]. This study compares the characteristics of an LLDPE/HDPE blend with an alumina nanocomposite under various processing circumstances utilizing a twin-screw extruder. Also, the analysis of the results will be used to discuss the differences in conductivity.
2. The Use Of Nanofillers In HVDC Cable
The study of fibered (particle) reinforced composites has shown that the characteristics of the composite are significantly influenced by the size of the filler material. This is because the size of the filler particle has a significant impact on surface interactions with the matrix, adhesion, particle motion, dispersion, and bonding. Because some of these effects become more pronounced as the filler size decreases, they have a greater impact on nanoscale characteristics. Because features like catalytic reactivity, electrical resistivity, adhesion, gas storage, and chemical reactivity are dependent on the structure of the interface, nanoscale fillers have a very large surface to volume ratio. [11]
In polymer blends, nanofillers can serve two purposes. The first is to improve mechanical, barrier, thermal, flame retardancy, and electrical qualities. Modification of miscibility/compatibility and morphology of polymer blends is the second. Immiscible polymer blends can have their morphology, interfacial properties, and performance changed by nanoparticles depending on where they are, how they interact with other polymer components, and how the additives spread throughout the polymer mixture. [12]
Nanotechnology has piqued the interest of people all across the world for more than two decades. The emergence of nanofillers and nanocomposites in both academic and industrial settings has added to this curiosity. The improved polymer composite properties of the nanosized particles have drawn the attention of several researchers over the years. Many
different types of nanofillers have been studied up till now. Among sensational nanofillers are silicon dioxide, SiO2, titanium dioxide, TiO2, graphene, C, aluminium dioxide, Al2O3, silicon nitride, Si3N4, boron nitride, BN.[13]
3. Two Level Factorial Design
To ascertain if particular elements determining the extent to which interactions between two or more factors have an impact on the response, whole two-level factorial designs are used. This is the subject of this chapter. These designs necessitate doing an experiment with all feasible mixes for each of the k components' two levels under consideration. Runs or treatments are two terms used to describe the studies. The latter expression comes from the study of agronomy, which invented many of the techniques used in experimental design. For example, one might look into the impact of adding phosphorus (P) and nitrogen (N) to a crop's yield. In its most basic form, P is for phosphorus (factor 1) and N is for Nitrogen (factor 2) that consist of 2 factors. For 2 factors, refer to Fig.1, it should be 4(22 ) number of responses. This necessitates the application of four distinct treatments to the crop (low P - low N, low P - high N, high P - low N, high P - high N). Fig. 1 shows two-level two-factor design experiments structure which the number of experiments were 4 (22 ). As shown in Fig. 2, two-level three factor design trials can also be taken into consideration which the number experiments are 8(32 ). In general, two experiments are necessary, where k is the number of elements. As a result, a complete 2 level factorial design is used to describe a two-level factor design. The levels can be depicted in a variety of ways. One common way is to write + (or + 1) for one level and - for the other (or - 1). When the factors are quantitative, the + level represents the greater value, the - level represents the lower value, and 0 represents the middle value. In this part, the 0 value will not be necessary. Qualitative elements are also represented by the notation. The + level is not always greater than the - level, but it differs from it, and the 0 level is rarely present. One common method is to designate one level as 0, and the other as 1. The pairing of + and - or 0 and 1 signifies an experiment. For instance, experiment + - shows that factor A was at the + level while factor B was at the - level.[14][15]
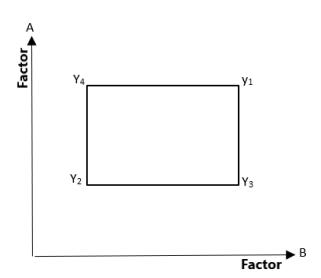
Figure 1. Factors A and B of a two-level, two-factor design
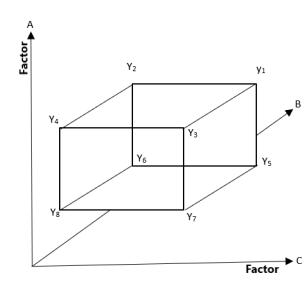
Figure 2. Factors A, B and C of a two-level, three-factor design
4. Twin Screw Extruder
The screw extruders are the most important processing tool utilized in the polymer industry and are essential in many related sectors. This project made use of twin-screw extruders. The
problem of mixing cellulose acetate without a solvent was addressed in Italy in the late 1930s by the development of a twin-screw extruder, a device with two single screws. Colombo successfully combined an extruder and a mixer using a system of co-rotating screws that interlock. [16] Compared to single screw extruders, twin screw extruders are more efficient at providing uniform mixing of a variety of materials, including additives, fillers, and liquids. Using mixing elements could increase the single screw extruder's mixing efficiency, but it would still fall short of twin-screw extruder efficiency. There are several types of twin-screw extruders that may be found, and they can be built differently. They can have parallel or conical screws that can rotate either counter-rotating or in the same direction as the screw's rotation. [17] The twin screw extruder was used in the experiment setting to create several sorts of samples for testing.
5. Methodology
A. Materials
Alumina in sizes ranging from 20 to 30 nm with LLDPE and HDPE is bought from suppliers. Injection moulding grade of linear low-density polyethylene (LLDPE) with a specified melt flow index of 2g/10min and density of 0.9170 g/cm3 was employed in this work. This resin was first offered by Itochu Chemicals America Inc. as extruded pellets. The high-density polyethylene (HDPE) injection moulding grade is designed to have a melt flow index of 10g/10min and a density of 0.956 g/cm3. This resin was initially offered by Lotte Chemical Titan (M) Sdn Bhd as extruded pellets. The combinations are composed in a 70:30 ratio of nanofiller, 70% LLDPE, and 30% HDPE.
B. Experimental Design
The two-level factorial design of experiment was conducted using the Design Expert Software (Statistics Made Easy, version 10.0.0.3, Stat-Ease, Inc., Minneapolis, MN). Both screening factor and optimization factor experiments were conducted to get the ideal LLDPE/HDPE concentration ratio using Alumina nanofillers. The main idea here is to strengthen the dielectric strength of the insulator by optimizing the concentration ratio of LLDPE/HDPE and Alumina. The enhancement in the conductivity properties is then reflected by the crystallinity of the sample.
B.1. Preparation And Testing Of The Polymer Nanocomposite
In this study, it begins with the preparation of sample LLDPE/HDPE-Alumina. The concentration of the LLDPE/HDPE is within the ratio 70:30 with 70 percent of LLDPE and 30 percent of HDPE [4] combine with the concentration of alumina with 1% and 5% wt. The concentration levels of mixed nanofiller are based on the design of experiment (DOE) using two level factorial design with the minimum value is 1% wt and the maximum value is 5% wt. The selection of the minimum maximum value is considering based on the effect from the filler to the blending with the lowest to the highest weightage percentage that could make an optimum results. Following this, the nanofiller were design with the screwspeed of the machine and also with the temperature varies. Using 1 and 5 weight percents of alumina, the mixing nanofiller was adjusted. One kilogram's worth of material is made up of 50 grammes of alumina, 70 grammes of LLDPE, and 300 grammes of HDPE with combination of 70:30:5. Some combinations have multiple ratios with the same value [18]. Given that mixing produces eutectic blends, a base polymer with a composition of 70LLDPE:30HDPE was chosen. [19] Moreover, it has superior mechanical and electrical performance compared to other thermoplastic materials. [20]. The twin screw extruder was used in the experiment setting to create several sorts of samples for testing. The variable setup for the screw speeds were determine at 65 and 75, while the temperatures were determined at 170o C and 180o C as shown in Table 1. Fig.3 shows the typical image of the compounding prepared from the twin screw extruder. The extruded samples were pelletized into small granules. The twin screw extruder's blend composition was heat-pressed from granules to square samples at a temperature of 170°C
to 180°C. For each blend composition, square samples with dimensions of 15 cm x 15 cm and a thickness of 1 and 3 mm were prepared. For each blend composition, 5 samples are prepared. Samples in a round form with a thickness of 1 mm and a diameter of 28 mm were made for the conductivity measurement test
B.2. Two Level Factorial Design
For the screening factor experiment, the 22 factorial design was employed to demonstrate the statistical significance of mixing LLDPE, HDPE with the Alumina nanofiller. The 2 factorial design was carried out for two independent variables with three replications which leads to eight set of experiment shows in table 1. A half-normal plot and an effect list were used to study the impacts of the independent variables on the conductivity based on the results of the experiment. Analysis of variance (ANOVA) was used to evaluate the suitability of the factorial model.
| LLDPE (%) | HDPE (%) | Nanofiller (%) | Screw Speed (rpm) | Temperature (OC) | Design | |
| 70 | 30 | 1 | 60 | 170 | A1 | |
| 70 | 30 | 1 | 75 | 170 | A2 | |
| 70 | 30 | 1 | 60 | 180 | A3 | |
| 70 | 30 | 1 | 75 | 180 | A4 | |
| 70 | 30 | 5 | 60 | 170 | A5 | |
| 70 | 30 | 5 | 75 | 170 | A6 | |
| 70 | 30 | 5 | 60 | 180 | A7 | |
| 70 | 30 | 5 | 75 | 180 | A8 | |
Table 1. Formulation and Identification Of Compounds
Figure 3. Output blending granules from the twin-screw extruder
C. Data Analysis
C.1. Conductivity Test Using 4-Point Probe
A straightforward tool for determining the conductivity of semiconductor samples is a fourpoint probe with the standard of ASTM-F1529-97 [21]. The substrate resistivity can be measured by running a current through two of the outer probes and measuring the voltage through the inner probes. The inner voltage probes experience an induced voltage as a result of a current flowing through the outer probes. The intersection of n- and p-type materials acts as an insulating layer, and the cell needs to be kept away from light. [22] Using this probe in conjunction with the K16220 software to capture the data, the conductivity of the samples was assessed for this investigation. For each operating frequency, the impedance was noted. The conductivity value was derived from the value impedance data, which also included the resistance values. The setup and preparations for the test are shown in Figure 4. Each sample
was 1mm thick and had an overall diameter of 2.8 cm. The formula (1) below was used to determine the conductivity value. [23],
\[\sigma = \frac{t}{RbA} \tag{1}\]
Where A = test sample's area, t = thickness Rb = resistance σ = conductivity.
Diagram of 4-point probe (b) Actual
Figure 4. Conductivity Test setup
C.2. Crystinallity Test Using Differential Scanning Calorimetry
Comparative Scanning With the test setup depicted in Fig. 5, calorimetry is a thermal analysis technique that measures the heat flow into or out of a sample. The entire sample is exposed to a regulated temperature program that changes as a function of time or temperature. The system detects the endothermic and exothermic transition like the determination of transformation temperature of solids as a function of temperature. The most important effects that can be analyzed by this system are melting point, melting range and melting behavior.
The sample that was being examined was put on an aluminium pan, and its weight was between 3-5 mg. Using an oxygen flow rate of 50 ml/min, heating the sample and reference pan to the same test temperature within a range of 170-210°C. The specimen's heat output was measured and kept track of. In DSC, the reference (often an empty metal pan) and the sample both rest on raised platforms on the sensors. Area thermocouples track the differential heat flow to the sample and reference as heat moves through the sensor. Sample temperature is controlled by a thermocouple. To further stabilize the baseline and provide the desired sample/atmosphere interaction, a warmed purge gas is present. In this study, polyethylene sample sets are examined at temperatures ranging from room temperature to 200 °C. The sample was heated at a rate of 10 °C/min while being surrounded by a nitrogen environment. Since a polymer's previous thermal history influences the measured degree of crystallinity, these samples are assessed both "as received" and after undergoing a standard "thermal treatment" meant to give all three samples an equivalent thermal history.
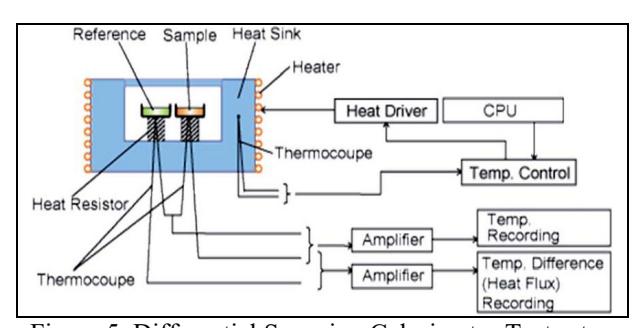
Figure 5. Differential Scanning Calorimetry Test setup
6. Result and Discussion
A. Conductivity Test
For each compounded sample, three samples were evaluated utilising three distinct line areas for the conductivity measurement using a 4-point probe and the K16220 software. For each compounding sample, the average value was calculated after the findings were recorded in Fig. 6. According to the graph, the maximum resistivity for sample A7, which contains 5 wt% alumina nanofiller, was measured at 180 o C temperature and 60 rpm of the screw speed extruder, respectively. Sample A2 has the lowest resistivity, which contains 1 wt% alumina and operates at 170 o C with a 60 rpm screw. The graph demonstrates that the resistivity increases from the virgin through A1, increases from A2 to the maximum at A7, and then starts to diminish once more at A8. Sample A7 is regarded as having the LLDPE/HDPE-Alumina nanocomposite's ideal composition, which results in the material's increased resistivity. The conclusion is that resistance strength rises as temperature rises. The dependency of conductivity on temperature or the electric field allows for the differentiation of several conductivity mechanisms.
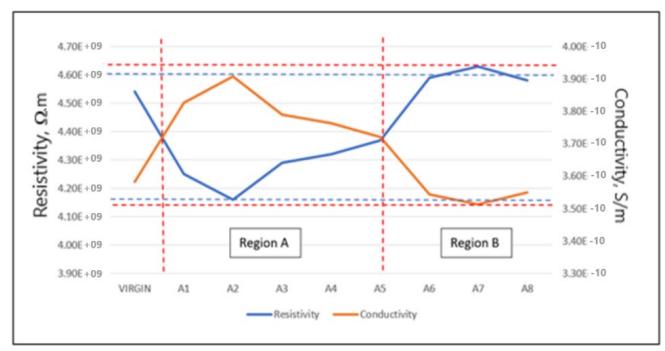
Figure 6. Resistivity and conductivity results of the LLDPE/HDPE-Alumina
Because conductivity is 1/resistivity, the situation in conductivity graphs is shown in the same graph. The sample has the best conductivity while searching for the best insulation in high voltage due to the composites' increased resistance. A lot of interest is being directed to polymer nanocomposites (NCs), which are composites of organic polymers and evenly dispersed nm-sized inorganic fillers. NCs are new materials with improved qualities in many different industries. According to recent research, polymers' dielectric properties, including as conductivity, space charge behaviour, breakdown strength, and resistance to partial discharge, are improved by the addition of nanofillers. [24]. Because alumina has a higher thermal conductivity property by nature, increasing the amount of alumina helps to dissipate heat, which lowers the dissipation factor [18]. The carriers aiding in charge of transportation have a significant impact on the conductivity of dielectric material. Hence, it is crucial to reduce the concentration of charge carriers, and insulation material needs to be thoroughly chemically and physically cleaned [25]. It can be seen from Fig. 8 that the outcome can be separated into two regions. Although region B contains samples with high resistivity and low conductivity and 5% wt of alumina nanofiller, region A contains samples with low resistivity and high conductivity. A good high voltage insulation cable needs to have low conductivity, hence area B is the ideal selection sample to use.
The results show that the sample's dielectric properties can vary depending on the amount of nanofiller injected. The resistivity of the sample is increased by the 5% wt of alumina nanofiller whereas it is decreased by the 1% wt of alumina nanofiller. By including 5% of alumina nanofillers at a temperature of 180°C and a screw speed of 60, it is possible to increase conductivity and resistivity percentages relative to a virgin polymer blend by 1.96% and 1.98%, respectively.
B. Screening Factor Experiment (Based on Conductivity)
The effect list and half-normal plot produced by the 22 factorial design utilised for the screening factor experiment are displayed in Table 2 and Fig. 7, respectively. The position of components A (weightage), B (temperature), and C (screw speed) in relation to the straight line is depicted in Fig. 9. Seeing that none of the variables resemble the straight line is interesting. The figure highlights the significance of model terms A, B, and C. This conclusion is indeed supported by the effect list, which demonstrates that variable A is the most important factor with a contribution of 73.67%. The sum of squares (SS) for this variable is 9.03125E-08. Factor B with a contribution of 15.51%. and SS of 1.90125 E-08, factor C with contribution of 5.40% and SS of 6.6125 E-09. This is followed by interaction AB, AC, BC and ABC with less than 3% contribution and SS less than 4E-0.9. Based on the results, it is evident that factor A (weightage) has a significantly higher contribution on the conductivity compared to factor B,C and the interaction. However, the contribution of other factors is still considered important.
| Table 2. List of Effects for Each Model Term In The Screening Factor Experiment |
|---|
| Term Intercept | Standardize effect | Sum of square | % Contribution |
|---|---|---|---|
| A - weightage | -0.0002125 | 9.03125E-08 | 73.67 |
| B - Temperature | -9.75E-05 | 1.90125E-08 | 15.51 |
| C - Screw speed | -5.75E-05 | 6.6125E-09 | 5.40 |
| AB | -1.25E-05 | 3.125E-10 | 0.25 |
| AC | -3.25E-05 | 2.1125E-09 | 1.72 |
| BC | 4.25E-05 | 3.6125E-09 | 2.95 |
| ABC | 1.75E-05 | 6.125E-10 | 0.50 |
Table 3 summarizes the ANOVA result analysis in term of degrees of freedom (df), sum of squares (SS), mean squares (MS), F-value, and p-value. The p-value that indicates the probability that the null hypothesis is true is 0.0054 which make the total regression model is significant. The p-value is less than 0.05, factors A (weightage) and B (temperature) are significant model variables (0.0018 and 0.0277 for factor A and factor B, respectively). Factor C (screwspeed) has a p-value of 0.1169 (which is greater than 0.05), indicating that this model component is not significant. Based on the ANOVA results, it can be revealed that the factor C (screwspeed) does not contributing to the significant effect of the material conductivity. Factors A and B are significantly contributed to the conductivity effect of the material as the pvalue less than 0.05.
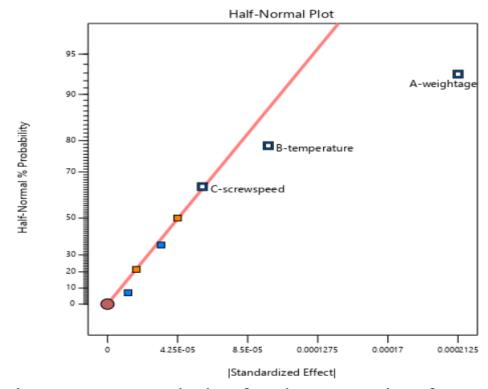
Figure 7. Normal plot for the screening factor
| Table 3. Results of The Factorial Model's ANOVA | ||||||
|---|---|---|---|---|---|---|
| Source | Sum of Square | df | Mean Square | F-Value | p-Value | |
| Model | 1.159E-07 | 3 | 3.865E-08 | 23.25 | 0.0054 | Significant |
| A-Weightage | 9.031E-08 | 1 | 9.031E-08 | 54.32 | 0.0018 | |
| B-Temperature | 1.901E-08 | 1 | 1.901E-09 | 11.44 | 0.0277 | |
| C-Screw speed | 6.613E-09 | 1 | 6.613E-09 | 3.98 | 0.1169 | |
| Residual | 6.650E-09 | 4 | 1.663E-09 | |||
| Cor Total | 1.226E-07 | 7 | ||||
Table 3. Results of The Factorial Model's ANOVA
The statistical significance of the model is shown by its F-value, which is 23.25. A 0.54 percent possibility of noise causing an F-value of this size to occur. P-values for significant model terms are less than 0.0500. The model terms A and B are critical in this situation. If the value is higher than 0.1000, the model terms are irrelevant. If a model has many terms that are not necessary, except from those that support hierarchy, model reduction may improve the model.
C. Optimization (Based On Conductivity)
Using the data from the 4-point probe experiment, the optimization factor experiment was carried out for various processing conditions during compounding with twin screw extruder. The conductivity of each sample was measured and computed, and the experiment's results were analysed using ANOVA. Equation (2) gives the final equation in terms of coded factors, while equation (3) gives the final equation in terms of real factors, showing the weightage of the nanofiller (x) and the temperature (y) of the processing condition. It should be noted that the regression equation includes all factors, regardless of their significance.
\[\sigma = +3.696e^{-0.10} - 1.062e^{-0.11}x - 4.875e^{-0.12}y\] (2)
Using the equation in terms of coded factors, it is possible to predict the response for a specific level of each factor. The coded equation can be used to compare the factor coefficients and ascertain the relative effects of the factors. The factor's high level is by default coded as +1, while its low level is coded as -1.
\[\sigma = +5.56188e^{-010} - 5.3125e^{-012}x - 9.75e^{-013}y\] (3)
Making assumptions regarding the outcome of specific levels of each element can be done using the equation expressed in terms of actual factors. Here, each factor's levels must be stated in their original units. As the intercept is not close to the design space's center and the coefficients are scaled to fit each factor's units, it is not advisable to use this equation to determine the relative weights of the various factors.
The conductivity of the sample is predicted using Equation (3) for each experimental data point is given in Table 4, also with the experimental data for comparison. Table 4 illustrates the applicability of this model, and it is clear that the majority of the predicted values are reasonably similar to the experimental values.
Table 4. Observed and predicted values
| Run order | Actual Value | Predicted Value | Residual |
| 1 | 3.8E-10 | 3.9E-10 | -0.0000 |
| 2 | 3.8E-10 | 3.8E-10 | 6.250E-06 |
| 3 | 3.6E-10 | 3.5E-10 | 8.750E-06 |
| 4 | 3.6E-10 | 3.6E-10 | -0.0001 |
| 5 | 3.7E-10 | 3.6E-10 | 0.0001 |
| 6 | 3.8E-10 | 3.8E-10 | 6.250E-06 |
| 7 | 3.9E-10 | 3.9E-10 | 0.0000 |
| 8 | 3.5E-10 | 3.5E-10 | -0.0000 |
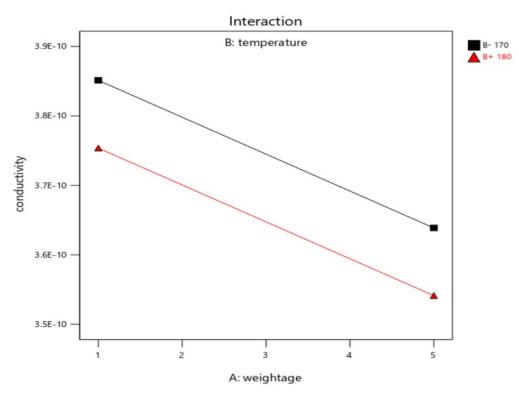
Figure 8. Interaction of the factor
Fig. 8 depicts the interaction plot of the LLDPE/HDPE-Alumina concentration conductivity level as a function of weightage and temperature for the processing condition during compounding with twin screw extruder. The conductivity value of the sample reduces as the weightage of the alumina nanofiller is increased from 3.75E-10 to 3.55E-10, and it also lowers while the temperature of the processing condition is increased. When the filler weightage is increased from 1wt percent to 5wt% percent, the conductivity of the LLDPE/HDPE-Alumina decreases progressively, while the conductivity decreases when the temperature is increased from 170o C to 180o C. This condition is also depicted in Fig. 9, which depicts the LLDPE/HDPE-Alumina sample's response surface plot as a function of weightage and temperature processing parameters. When the filler weightage and processing temperature are both 5 wt% and 180o C, the minimum conductivity of 3.5E-10 is achieved.
The study discovered that the optimal composition for lowering the material's conductivity is created by adding 5% weight Alumina to the LLDPE/HDPE polymer. How the matrix and filler interact with one another is determined by the chemical characteristics of the filler surface and the interfacial region. The free zone of the substance had received the nanofiller injection. Because of their poorer conductivity, alumina nanofillers have dielectric properties. [26]
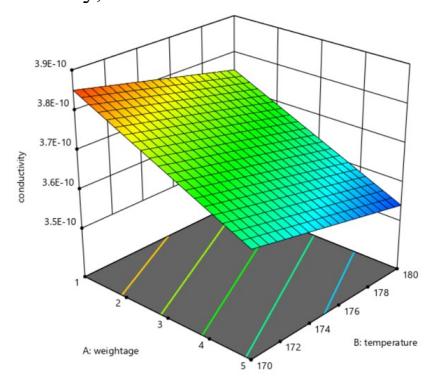
Figure 9. Respond surface plot
D. Crystallinity Result
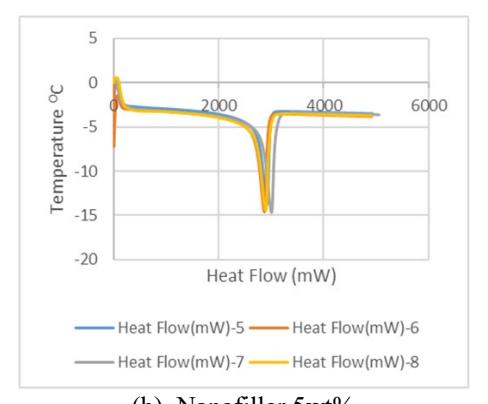
Fig.10 shows the melting endotherm for all of the LLDPE/HDPE-Alumina samples during the initial "as received" heating. Figure 10(a) shows the melting endotherm for sample A1 - A4 while the figure 13(b) shows the melting endotherm for sample A5 - A8. From the observation, the peak for A3 and A4 are higher than others sample. Based on 270.03 J/g for the 100% crystalline material, the percentage of crystallinity is calculated using Universal Analysis software. Table 5 provides an overview of the findings for the analysed samples. These findings clearly show that samples A3 and A7 share the same melting profile and crystallinity,
indicating that these two polymers were previously processed under the same conditions in the twin screw extruder (with the temperature of 180OC and screw speed of 60 rpm). The decreased crystallinity of other samples, on the other hand, indicates different processing circumstances and various end-use qualities. By measuring the enthalpy of fusion and normalizing it to the enthalpy of fusion of a 100% crystalline polymer, DSC can rapidly and easily assess the degree of crystallinity of thermoplastic polymers. The typical precision is a few percent.
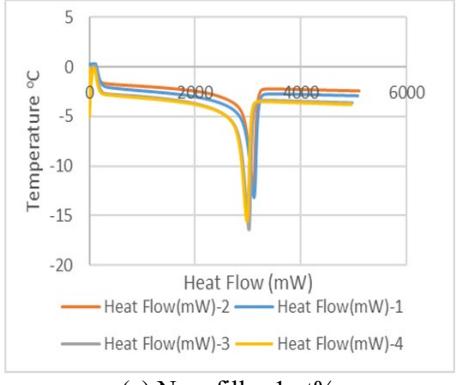
(a) Nanofiller 1wt%
(b) Nanofiller 5wt%
Figure 12. Heat Flow of LLDPE/HDPE-Alumina
Table 5. Crystallinity of LLDPE/HDPE-Alumina
| Tm (OC) | ∆Hm (J/g) | ∆Ho (J/g) | Crystinality (%) | |||
| A1 | 128.56 | 103.8 | 270.03 | 38.44 | ||
| A2 | 128.38 | 98.64 | 270.03 | 36.53 | ||
| A3 | 128.24 | 115.5 | 270.03 | 42.77 | ||
| A4 | 127.68 | 105 | 270.03 | 38.88 | ||
| A5 | 127.31 | 88.32 | 270.03 | 32.71 | ||
| A6 | 127.68 | 98.54 | 270.03 | 36.49 | ||
| A7 | 128.3 | 107.2 | 270.03 | 39.70 | ||
| A8 | 128.73 | 101.9 | 270.03 | 37.74 | ||
7. Conclusion
The conductivity characteristics of polymer blends were examined using various compounding processes in the section above. As a result, the blend's conductivity was discovered to be relatively unique from the others. Considering the outcomes of the 4-point probe test, adding extra alumina at a specific percentage will enhance the LLDPE/HDPEdielectric Alumina's characteristics. It has been discovered that the polymer blend with 5 weight percent of alumina nanofiller is the ideal composition for HVDC insulation, having the highest resistance and lowest conductivity. The compounding variable is another element that improves the dielectric characteristics. According to the results, the composition becomes more stable around 180 °C. In this work, the design of experiment (DOE) is demonstrated to be a beneficial approach for determining the best processing condition for sampling the compounding of LLDPE/HDPE-Alumina, which helps to increase the conductivity of the polymer nanocomposite with a percentage contribution of 73.67 % for the weightage effect factor. The DOE method allows researchers to identify the factors that have a substantial impact on the conductivity of LLDPE/HDPE-Alumina with fewer test runs, as demonstrated by the percentage contribution of each component. This method saves a lot of time and money when compared to command approach, which is a one-factor-of-a-time (OFAT) method. The ideal weightage concentration and temperature for the LLDPE/HDPE-Alumina that gives the lowest conductivity level are 5 wt% and 180 OC, respectively, according to the response surface plot. The p-value is 0.0054 and the model F-value is 23.25, make the overall regression model is significant. An F-value of this magnitude has a 0.54 percent chance of occurring due to noise. Ultimately, it's possible to conclude that conductivity tests can be used to compare the dielectric properties. Various nanofiller types and concentration levels will result in varying conductivity and current values. It can be seen that variations in twin screw extruder processing conditions have a tendency to vary conductivity values.
8. Acknowledgment
The usage of facilities and financial assistance were greatly appreciated by the authors by the Universiti Sains Malaysia (USM), Universiti Malaysia Perlis (UniMAP) and Malaysia Ministry of Higher Education (MOHE).
9. References
- [1]. Y. Zhou, S. Peng, J. Hu, and J. He, "Polymeric insulation materials for HVDC cables: Development, challenges and future perspective," IEEE Trans. Dielectr. Electr. Insul., vol. 24, no. 3, pp. 1308–1318, 2017, doi: 10.1109/TDEI.2017.006205.
- [2]. M. F. Frechette et al., "Nanodielectrics: A "universal" panacea for solving all electrical insulation problems?," pp. 1–3, 2010, doi: 10.1109/icsd.2010.5568070.
- [3]. C. W. Reed, "An assessment of material selection for high voltage DC extruded polymer cables," IEEE Electr. Insul. Mag., vol. 33, no. 4, pp. 22–25, 2017, doi: 10.1109/MEI.2017.7956629.
- [4]. Z. Kai et al., "The mechanical properties of recyclable cable insulation materials based on thermo-plastic polyolefin blends," Proc. IEEE Int. Conf. Prop. Appl. Dielectr. Mater., vol. 2015-Octob, pp. 532–535, 2015, doi: 10.1109/ICPADM.2015.7295326.
- [5]. K. Zhang, L. Zhong, J. Gao, L. Li, L. Cao, and G. Chen, "Temperature dependence of crystalline structure and DC performance in LLDPE/HDPE blending material," IEEE Trans. Dielectr. Electr. Insul., vol. 26, no. 3, pp. 754–759, 2019, doi: 10.1109/tdei.2018.007652.
- [6]. N. A. M. Jamail et al., "Effect of nanofillers on the polarization and depolarization current characteristics of new LLDPE-NR compound for high voltage application," Adv. Mater. Sci. Eng., vol. 2014, 2014, doi: 10.1155/2014/416420.
- [7]. G. Zhang et al., "Preparation of polymer / clay nanocomposites via melt intercalation under continuous elongation fl ow," Compos. Sci. Technol., vol. 145, pp. 157–164, 2017, doi: 10.1016/j.compscitech.2017.04.005.
- [8]. W. U. Shishan, J. Dingjun, and O. Xiaodong, "The Structure and Properties of PA6 / MMT Nanocomposites," vol. 44, no. 11, pp. 2070–2074, 2004, doi: 10.1002/pen.20211.
- [9]. C. T. Ratnam, K. Zaman, M. Nasir, and A. Baharin, "Effect of Blending Temperature on the Mechanical Properties of Pvc / Enr Blend Upon Irradiation Inis-My--045," no. M.
- [10]. L. Incarnato, P. Scarfato, G. M. Russo, L. Di Maio, P. Iannelli, and D. Acierno, "Preparation and characterization of new melt compounded copolyamide nanocomposites," vol. 44, pp. 4625–4634, 2003, doi: 10.1016/S0032-3861(03)00360-4.
- [11]. E. I. Akpan, X. Shen, B. Wetzel, and K. Friedrich, Design and Synthesis of Polymer Nanocomposites. Elsevier Inc., 2018.
- [12]. R. Scaffaro and L. Botta, Nanofilled Thermoplastic-Thermoplastic Polymer Blends. Elsevier Inc., 2013.
- [13]. M. S. Khalil and J. A. Jervase, "Development of polymeric insulating materials for HVDC cables using additives: evidence from a multitude of experiments using different techniques," Conf. Rec. IEEE Int. Symp. Electr. Insul., pp. 485–488, 2000, doi: 10.1109/elinsl.2000.845554.
- [14]. S. A. Ghani, N. A. Muhamad, H. Zainuddin, Z. A. Noorden, and N. Mohamad, "Application of response surface methodology for optimizing the oxidative stability of natural ester oil using mixed antioxidants," IEEE Trans. Dielectr. Electr. Insul., vol. 24, no. 2, pp. 974–983, 2017, doi: 10.1109/TDEI.2017.006221.
- [15]. P. Whitcomb, "Chapter 5 Two-level factorial designs," Data Handl. Sci. Technol., vol. 24, no. C, pp. 87–117, 2005, doi: 10.1016/S0922-3487(05)80009-7.
- [16]. "Co-Rotating Twin-Screw Extruders," in Co-Rotating Twin-Screw Extruder, 2007.
- [17]. A. Shrivastava, "Introduction to Plastics Engineering," in Introduction to Plastics Engineering, 2018.
- [18]. R. Ramkumar and C. P. Sugumaran, "Investigation on dielectric properties of HDPE with alumina nano fillers," 2016 IEEE 7th Power India Int. Conf. PIICON 2016, pp. 1– 4, 2017, doi: 10.1109/POWERI.2016.8077207.
- [19]. L. Lunzhi et al., "Dielectric behaviors of recyclable thermo-plastic polyolefin blends for extruded cables," Proc. IEEE Int. Conf. Prop. Appl. Dielectr. Mater., vol. 2015-Octob, pp. 180–183, 2015, doi: 10.1109/ICPADM.2015.7295238.
- [20]. L. Li, L. Zhong, K. Zhang, J. Gao, and M. Xu, "Temperature dependence of mechanical, electrical properties and crystal structure of polyethylene blends for cable insulation," Materials (Basel)., vol. 11, no. 10, 2018, doi: 10.3390/ma11101922.
- [21]. W. Conshohocken, "Standard Test Method for Sheet Resistance Uniformity Evaluation by In-Line Four- Point Probe with the Dual-Configuration Procedure," Am. Soc. Test. Mater., pp. 1–12, 1997.
- [22]. C. Honsberg and S. Bowden, "pveducation.org," pveducation.org, 2018. .
- [23]. S. N. I. Omar et al., "Electrically conductive fabric coated with polyaniline: physicochemical characterisation and antibacterial assessment," Emergent Mater., vol. 3, no. 4, pp. 469–477, 2020, doi: 10.1007/s42247-019-00062-4.
- [24]. J. Katayama, N. Fuse, M. Kozako, T. Tanaka, and Y. Ohki, "Comparison of the effects of nanofiller materials on the dielectric properties of epoxy nanocomposites," Annu. Rep. - Conf. Electr. Insul. Dielectr. Phenomena, CEIDP, pp. 318–321, 2011, doi: 10.1109/CEIDP.2011.6232660.
- [25]. G. Chen, J. T. Sadipe, Y. Zhuang, C. Zhang, and G. C. Stevens, "Conduction in linear low density polyethylene nanodielectric materials," Proc. IEEE Int. Conf. Prop. Appl. Dielectr. Mater., pp. 845–848, 2009, doi: 10.1109/ICPADM.2009.5252208.
- [26]. B. Wunderlich, "Thermal analysis of polymers," Journal of Thermal Analysis. 1973, doi: 10.1007/BF01914481.
Syatirah Mohd Noor received the B.Eng. degree in Industrial Electronic engineering and the M.Eng. degree in Electrical Engineering from the Universiti Malaysia Perlis, Perlis, Malaysia, in 2008 and 2011, respectively. She is currently a Lecturer with the Faculty of Electrical Engineering Technology, Universiti Malaysia Perlis, Malaysia. Her research interests include Design of Experiments, Insulation in HVDC cable, Electrical Machine Design and Power Electronic
Mohamad Kamarol Mohd Jamil (senior Member,IEEE) (M'10–SM'19) received his B.Eng. degree (Hons) in Electrical Engineering from Universiti Technology Mara, Malaysia, in 2000, M.Eng. degree from the Kyushu Institute of Technology, Japan in 2005 and the D.Eng. degree in 2008. Within his doctor course study, he received the Chatterton Young Investigator Award from the IEEE International Symposia on Discharges and Electrical Insulation in Vacuum in 2006. In 2002, he joined Universiti Sains Malaysia (USM) with a University ASTS Fellowship. He was later been a
Senior Lecturer in 2008 and was promoted to Associate Professor in 2014.
He was a Senior Engineer at Sankyo Seiki (M) Sdn. Bhd. for almost 8 years. He was a Visiting Researcher with the High Voltage Laboratory, Kyushu Institute of Technology, Japan from 2013 to 2014 and Chiba Institute of Technology, Japan, from Feb, 6-20, 2020. His research interests include the insulation properties in oil palm, solid dielectric material, insulation properties of environmentally benign gas, and PD detection technique for insulation diagnosis of power apparatus and electrical machine. He is also involved in temperature rise and shortcircuit electromagnetic study of busbar system and HVDC system. He is a Professional Engineer and Chartered Engineer, and a member of the IET, the Board of Engineers Malaysia and the Institution of Engineers Malaysia.
Nor Asiah Muhamad (M'13) is currently serving as Senior Assistance Professor at Faculty of Engineering Universiti Teknologi Brunei, at same time she also serve as Associate Professor at the School of Electrical and Electronic Engineering, Universiti Sains Malaysia. Previously, she was a researcher and senior lecturer at the Institute of High Voltage and High Current (IVAT) in the Faculty of Electrical Engineering, Universiti Teknologi Malaysia. She obtained her PhD degree in 2009 from the University of New South Wales, Australia. She received her Bachelor's
degree in Electrical and Electronic Engineering from Universiti Teknologi Petronas, Malaysia, in 2002 and a Master's degree in Electrical Power Engineering from the University of South Australia in 2006.
She also obteined Chartered Engineer from UK Engineering Council since 2013, Professional Engenieur from BEM Malaysia since 2017 and Restricted- Competent (100kV) Person from Malaysia Energy Commision since 2020. Her research interest is centred on power system equipment monitoring, in particular, insulation diagnosis and the development of new systems for condition monitoring. Besides doing research in the HV area, she also works in energy efficiency and integration for a domestic and industrial areas in Malaysia.
Sharin Ab Ghani received his BEng. (Hons.) degree in Electrical Engineering from UTeM in 2008, M.Eng. Degree in Electrical Engineering from Universiti Tenaga Nasional in 2012, and Ph.D. degree in Electrical Engineering from Universiti Teknologi Malaysia in 2019. Currently, he is serving as Senior Lecturer at Faculty of Electrical Engineering, Universiti Teknikal Malaysia Melaka. His research interests are centered on high voltage engineering, power equipment condition monitoring, green electrical insulation, design of experiments, and optimization. To date, his outstanding
research works have been published in WoS-SCI (3) and Scopus (29) indexed journals. He also has experience in consultation work with industries related to electrical installation design, transformer condition assessment, and partial discharge analysis. He can be contacted at email: sharinag@utem.edu.my.
Khairul Anwar Abdul Halim is a Senior Lecturer in School of Materials Engineering, Universiti Malaysia Perlis. He has expertise in material characterization and testing in particular establishing structure-property relationship of materials. Completed PhD at Athlone Institute of Technology, Ireland where during his research studies, he had worked with one of prominent medical devices company that produce balloon for angioplasty application as part of research collaboration. Khairul Anwar has published papers in nanocomposite materials area for biomedical applications and
conductive polymer composites. Had participated and won several international and local research exhibitions. He is a currently working on conductive polymer composites for flexible electronic interconnect applications under Fundamental Research Grant Scheme (FRGS) as lead researcher. He is also a research associate in nanomaterials group under Centre of Excellence Geopolymer and Green Technology.